

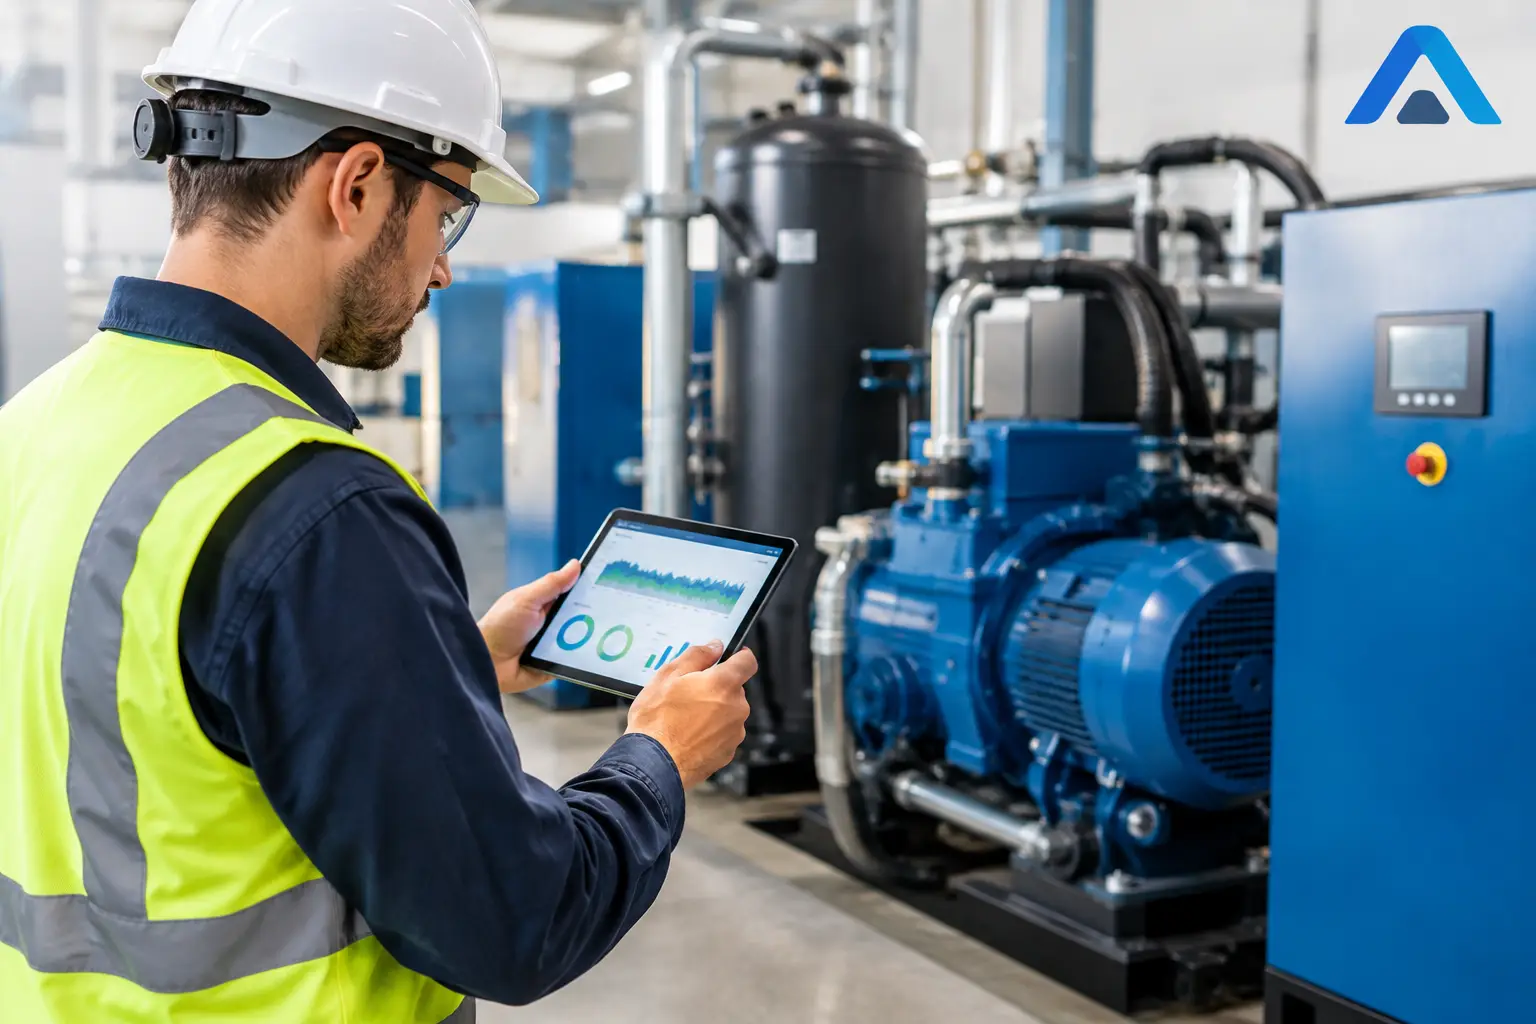
A compressed-air system can consume a significant share of a factory’s electricity while remaining largely invisible in routine energy reports. The compressor may appear to be operating normally, yet pressure setpoints, air leaks, unloaded running and peak-period loading can quietly inflate monthly costs. Knowing how to monitor compressor energy turns that hidden consumption into a controllable operational variable.
For industrial and commercial sites, the objective is not simply to record kilowatt-hours. It is to understand when, where and why compressed air is consuming electricity, then use that insight to reduce avoidable demand without compromising production or air quality.
Start with the electrical and operating picture
A useful monitoring programme begins at the compressor incomer, not at the main site meter. Install revenue-grade or suitably specified sub-metering for each major compressor, including current transformers and voltage measurement where required. This provides true power in kW, energy in kWh, power factor and demand data at the asset level.
Electrical data must be paired with operating data. At a minimum, capture running status, loaded and unloaded status, discharge pressure, run hours, alarms and ambient conditions. For variable-speed compressors, also monitor speed or output where the controller makes it available. Without these operating signals, a rise in energy use is difficult to distinguish from a legitimate increase in compressed-air demand.
Air flow measurement adds another layer of value, particularly for high-consumption systems. It enables the site to calculate specific energy consumption, usually expressed as kWh per cubic metre of air delivered. This metric reveals whether the system is producing compressed air efficiently, rather than merely consuming less power during lower production periods.
How to monitor compressor energy with the right KPIs
A dashboard crowded with readings does not create better decisions. Energy, engineering and facilities teams need a concise set of indicators that connects compressor performance to cost and operational risk.
Track energy consumption in kWh by compressor, production area and shift. Compare this with power demand in kW, especially during the site’s maximum-demand periods. A compressor starting or loading at the wrong time can create a costly demand spike even if its total daily energy use appears reasonable.
Also monitor specific energy consumption, average discharge pressure, loaded versus unloaded hours, and compressor sequencing. High unloaded hours indicate that a fixed-speed machine is drawing substantial power without delivering useful air. A pressure band that is wider than necessary may point to poor control, excess storage requirements or instability elsewhere in the network.
Production-normalised data is essential. Energy per unit produced, per operating hour or per batch provides a fair comparison across shifts and seasons. If total compressor consumption rises because output rises, that may be expected. If energy per unit rises while output is stable, the site has a clear investigation point.
Establish a baseline before changing control settings
A baseline should cover representative production conditions, including weekdays, weekends, changeovers and any high-demand operating periods. For many sites, four to eight weeks of interval data is enough to identify recurring patterns, although complex facilities may require longer.
Review the baseline alongside production schedules, tariff windows, maintenance records and weather data. Ambient temperature affects compressor efficiency, while shifts in product mix can change air demand materially. A baseline that ignores these variables may lead to false savings claims or inappropriate control changes.
The best baseline identifies an achievable operating range, not one idealised number. Some processes genuinely require higher pressure, guaranteed standby capacity or continuous air supply. Monitoring should reveal waste without creating a control strategy that threatens process reliability.
Find the causes of avoidable consumption
Real-time data is most valuable when it leads to a defined operational response. A persistent overnight load can indicate air leaks, equipment left connected outside production hours, or a compressor held at pressure for an unnecessary period. A high minimum demand during non-production time is often one of the clearest leak-survey triggers.
Pressure is another common source of waste. Raising system pressure can mask poor network design or local pressure drops, but it also increases energy consumption and leakage rates. Before reducing the pressure setpoint, validate the critical end-use requirement and measure pressure at the point of use. The compressor discharge reading alone does not tell the full story.
Compressor sequencing deserves equal attention. Multiple machines operating independently may compete rather than share load efficiently. One unit may run unloaded while another trims demand, or a less efficient compressor may operate as the base-load machine. A central controller can improve sequencing, but its logic must reflect actual compressor performance, maintenance availability and the production risk profile.
Connect monitoring to demand and energy strategy
For high maximum-demand users, compressor monitoring should sit within the wider site energy picture. A compressor is rarely the only large load. Chillers, pumps, furnaces, HVAC equipment and process lines may coincide to create an expensive peak.
An enterprise energy-management platform can correlate compressor demand with whole-site load, solar generation and battery state of charge. This makes it possible to identify whether a compressor start sequence is contributing to an avoidable demand event and to plan a response. Depending on process constraints, the response may include rescheduling non-critical air demand, optimising compressor staging, prioritising solar consumption or dispatching a battery during a peak window.
This is where monitoring becomes smarter control. The decision is not always to switch equipment off. In a continuous-production environment, protecting uptime comes first. The better outcome may be to run the most efficient compressor at a stable load, avoid a simultaneous start with other major assets, and use stored energy to manage a short-duration peak.
Use alarms that prompt action, not noise
Set alert thresholds around events that need intervention: abnormal overnight baseload, prolonged unloaded running, pressure outside the approved band, unexpected energy intensity, repeated starts, or a mismatch between compressor run time and production schedules.
Alerts should be assigned to named operational owners with a practical response path. A facilities manager may investigate a pressure excursion, while production may need to confirm whether an out-of-hours air load is intentional. Finance and sustainability teams need verified monthly reports, not continuous alarm notifications.
A well-configured Management Reporting System can automate this workflow by presenting interval data, exceptions and cost-relevant performance trends in one view. Amsolar AI’s MRS approach can also incorporate environmental sensors, helping teams relate HVAC and compressor conditions to actual energy behaviour rather than reviewing isolated meter readings.
Turn findings into verified savings
The most credible compressor-energy projects measure savings after changes are made. Document the original operating condition, the intervention, the expected impact and the verification period. Typical actions include repairing leaks, reducing pressure where process validation permits, improving receiver capacity, revising sequencing, replacing inefficient equipment or adjusting operating schedules.
Compare post-change results against the production-normalised baseline, while accounting for material changes in output, weather and operating hours. This discipline matters for internal investment decisions, ESG reporting and compliance-focused energy reviews. Real savings, not theoretical estimates, give engineering, finance and sustainability leaders a shared basis for action.
Compressor energy monitoring is most effective when it becomes part of the operating rhythm: reviewed weekly by site teams, linked to monthly cost reports and used to guide capital planning. A meter alone cannot lower a bill. Clear data, accountable decisions and intelligent control can make compressed air a managed energy asset rather than a permanent source of hidden demand.